25373994391 Guide to Sourcing and Validation
25373994391-focused procurement guidance helps buyers evaluate components with practical sourcing, verification, and risk controls. Objectively, such numeric identifiers are commonly used in inventory systems for traceability, version control, and procurement workflows. This guide explains how to interpret identifiers, what to confirm with suppliers, and how to document requirements for reliable intake and compliance.
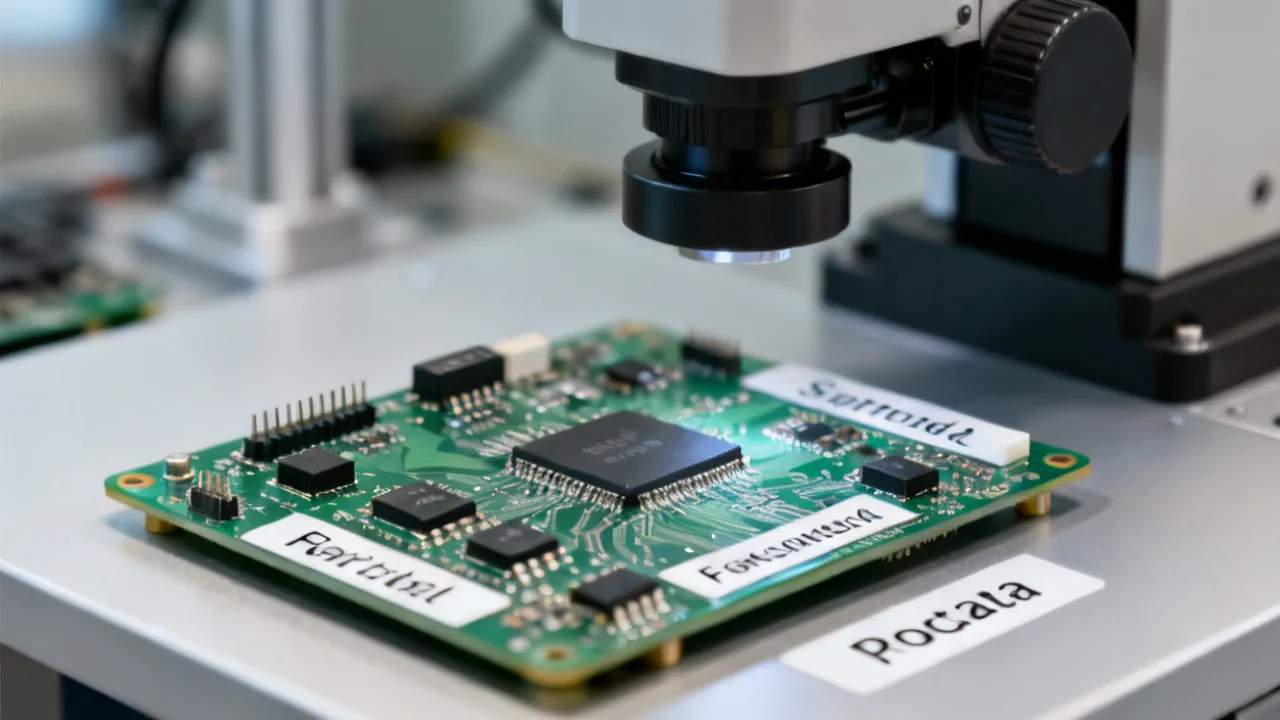
Immediate takeaways for sourcing and validating 25373994391
If you are dealing with 25373994391, treat it as an inventory and traceability anchor: the identifier should connect unambiguously to the correct part specification, manufacturer details, revision level, and packaging/handling assumptions. The safest procurement outcome comes from verifying the part’s exact identity (not just the number), confirming price and lead-time terms in writing, and maintaining a traceable intake record—especially when the supplier is your only source of configuration certainty.
In this article, you’ll see an expert-oriented approach to interpreting such identifiers and implementing quality checks throughout ordering, receiving, and verification. Although the numeric code is central to many supply workflows, it should never be the only control—substituting “number-only” decisions for specification confirmation is a common reason for returns, delays, and downstream mismatches.
Additionally, this is one of those situations where the right mindset matters as much as the checklist: you should assume the number might be “technically close” rather than “contractually identical” unless you force proof. That proof comes from the supplier’s documentation (what they say they shipped), from the label/markings (what they physically packaged), and from your own verification tests (whether it performs as required). Only when all three align should you release parts to production or to any process that cannot tolerate nonconformity.
Finally, remember that even a perfect number-to-spec mapping can fail at the edges: when packaging format changes, when reel size differs, when handling requirements (ESD, moisture sensitivity, temperature controls) are not met, or when revision control changes the manufacturing recipe while leaving the external identifier unchanged. Your procurement plan should address those edge cases upfront.
Why identifiers like 25373994391 matter in procurement
In very industrial procurement environments, a numeric string such as 25373994391 typically functions as a stable reference inside an ERP, warehouse label system, or supplier catalog mapping. In practice, the identifier is useful because it reduces ambiguity during purchasing, receiving, and troubleshooting. However, the identifier alone is insufficient unless it is tied to a controlled specification set: manufacturer name, model, revision, electrical/mechanical parameters, compliance declarations, and approved alternates (if any).
From an industry perspective, the top procurement systems treat an identifier as a pointer to documented truth: drawings, datasheets, revision histories, and quality documentation. When that pointer is not verified, teams may inadvertently order the “same-looking” item that behaves differently in production, or a “compatible” substitute that is not acceptable under contract or regulatory requirements.
Think of the identifier as the address and the specification bundle as the contents. Addressing errors are common when identifiers are reused across warehouses, or when distributors maintain multiple cross-references for legacy parts. Content errors are common when suppliers substitute revisions, use alternate sourcing, or package components differently (for example, tape-and-reel versus bag-and-box, or different ESD classifications). Procurement failures occur when teams trust the address without verifying the contents.
Moreover, identifiers like 25373994391 matter for more than receiving accuracy. They also become critical during:
- Root cause analysis: when a field return occurs, you must know exactly which revision and which lot you installed.
- Engineering change management: you need confidence that “the part number you bought” corresponds to the revision your design expects.
- Audit readiness: many audits ask for evidence that you controlled sourcing, verified conformance, and maintained traceability.
- Warehouse operations: stock rotation, quarantine handling, and internal transfers depend on consistent identity mapping.
So, 25373994391 is important not because it is magic, but because it is the pivot around which traceability and quality controls are organized. If you treat it as such, you can build a robust procurement workflow that scales even when suppliers change or demand is volatile.
What buyers typically miss when they focus only on 25373994391
Many procurement teams initially believe a part number is self-sufficient. In reality, several real-world issues can break that assumption:
- Revision drift: Two suppliers may map 25373994391 to different internal revisions or packaging.
- Variant confusion: The same base identifier might exist across voltage, tolerance, lead configuration, temperature rating, or lead finish variants.
- Documentation gaps: A supplier may provide no traceability paperwork, limiting your ability to pass internal QA or customer audits.
- Price-model mismatch: Unit price may be contingent on quantity breaks, lane availability, special handling, or compliance documentation scope.
- Substitution policy differences: some suppliers may “reserve the right” to substitute materials or manufacturing sites, even when the external part number is unchanged.
Therefore, an effective approach is to use 25373994391 as the starting point—then validate the specification bundle and commercial terms before release. In high-reliability manufacturing contexts, you should treat any “minor discrepancy” between your records and supplier documentation as a risk event that requires resolution before parts are issued to production.
Another frequently missed element is how procurement systems store mapping information. If your ERP or procurement catalog links 25373994391 to a manufacturer and revision, that mapping must itself be controlled—otherwise the number can remain “correct” in procurement while silently pointing to an outdated specification. The practical takeaway is that identity control includes both external verification (supplier proof) and internal master-data governance (your own controlled mapping).
Price discipline: how to discuss price without risking mis-buys
You asked to incorporate price information and supplier details, but the provided prompt contains blanks where those specifics would normally appear (for example, fields resembling empty strings). Because I cannot reliably insert unprovided pricing or vendor facts, the professional top practice is to structure your procurement conversation so that pricing is contextual and auditable.
When quoting or requesting a price for 25373994391, require clarity on at least these points:
- Pricing basis: price per unit, per reel/pack, or per lot (including whether packaging format is included).
- Quantity ladder: confirm how the price changes across your intended order size, including whether the ladder depends on lead time or allocation.
- Incoterms and delivery boundary: define responsibility for shipping, insurance, customs, and documentation (e.g., whether the quote is DAP/DDP or FOB).
- Lead time & availability: specify whether availability is “on-hand,” “allocated,” or “manufactured-to-order.”
- Return/replace terms: define the conditions for RMA if the delivered item fails verification (identity, revision, performance, or packaging/handling requirements).
- Compliance and test document scope: confirm whether CoC/CoA, test reports, or special certificates are included or excluded from the price.
- Excess/shortage rules: clarify how shortages are handled (replacement shipped? prorated? credits?) and whether substitutions are allowed.
This is how procurement professionals prevent the common scenario where buyers receive a “technically close” item but cannot justify returns because documentation and acceptance criteria were not locked before shipment. When price is discussed without explicit acceptance scope, suppliers may argue that the buyer accepted the goods by virtue of receiving and paying—making your QA disputes harder.
A useful discipline is to ensure that your purchase order (PO) ties the commercial terms to identity controls. For example:
- Use a PO line item that includes not only 25373994391, but also the manufacturer name, revision level, and any critical specs.
- Attach an acceptance criteria document (or at least specify the testing and inspection requirements).
- Include packaging requirements (e.g., moisture sensitivity handling, reel type, ESD labeling) as contract terms, not as “nice to have.”
In addition, you should avoid relying on vague phrases like “equivalent” or “compatible” without documentation. If the supplier wants to propose an alternate, require an engineering change approval process and written confirmation that the alternate satisfies the same acceptance criteria as the original.
Supplier verification: making the supplier accountable for identity
Because procurement often relies on supplier-provided mapping, the supplier should be held responsible for identity integrity. For 25373994391, your supplier verification should include:
- Manufacturer disclosure: confirm the actual manufacturer, not just the distributor or broker.
- Revision level and datasheet alignment: ensure the supplier’s datasheet revision matches your internal requirement.
- Packaging details: verify reel size, moisture barrier requirements (if applicable), handling instructions, and labeling format.
- Quality documentation: request CoC/CoA and, when required, test reports or inspection certificates.
- Lot or batch traceability: confirm that the supplier will provide lot numbers and that these will correspond to the documents included in shipment.
From an industry expert standpoint, the goal is to make the supplier’s statements verifiable through documents you can retain for audits, production traceability, and customer-facing commitments. You should also verify the identity chain for the entire supply route, not only the last supplier in your commercial relationship.
In practice, suppliers sometimes purchase through multiple levels of channels. Your verification plan should ask:
- Where are the parts manufactured?
- Are you sourcing from authorized distribution or from surplus / broker channels?
- Do you guarantee that the parts shipped correspond to the stated manufacturer and revision?
Then, align that supplier verification with contractual protections. Even if you trust the supplier, you need clauses that ensure your ability to return nonconforming items and claim replacement/credit when the delivered product does not match the verified documentation and your acceptance criteria.
Receiving and validation: a stepwise control plan
Once the order for 25373994391 arrives, control should shift from “commercial trust” to “measurable verification.” Below is an inverted-pyramid approach: start with the very critical checks, then move to supporting checks.
The stepwise plan matters because receiving inspection is not infinite in time or budget. Even so, you can design it so that the most identity-critical checks happen first, while lower-risk checks can be sampled more lightly.
Very critical: identity and spec conformity
Before you release parts to production (or to build work), confirm the delivered item identity against the approved spec:
- Label-to-order matching: ensure the shipment label references the same ordering identifier and includes correct revision/variant markings.
- Physical and dimensional checks: verify the form factor, key dimensions, pin/termination style, mounting features, mechanical interface, and any labeling/marking content required by the approved datasheet.
- Electrical/functional verification: perform at least sampling tests that demonstrate conformity to the datasheet parameters (e.g., resistance range, operating temperature behavior, insulation resistance, continuity, or other functional checks depending on the part type).
- Compliance documentation review: confirm any required declarations (e.g., conformity statements, RoHS/REACH where applicable) and retain the documents.
- Exception handling: define what happens if any critical identity marker is inconsistent (quarantine immediately; stop release; escalate to QA and procurement).
A strong identity check goes beyond “does it look right.” You want objective evidence that the delivered part corresponds to the exact spec and revision used in your product configuration.
Secondary: packaging integrity and traceability readiness
Even if the part appears correct, packaging and traceability failures can compromise your downstream processes:
- Moisture/ESD handling evidence: check for intact seals, correct desiccant indicators (where applicable), and ESD packaging quality (anti-static bags, correct labeling, damage-free cushioning).
- Lot/batch traceability: record lot numbers and link them to your internal receiving record for traceability.
- Condition at intake: document any damage, crushed packaging, missing labels, torn reels, or inconsistencies between packaging labels and paperwork.
- Label completeness: ensure the labels include required information (lot, quantity, part identifier, manufacturer, revision if required) so that traceability is preserved even after internal moves.
This is especially important when parts are stored for later use. If packaging is wrong, the parts might fail environmental requirements; if labeling is wrong, you lose your ability to prove what you installed later.
Documentation: how to build a defensible paper trail
For high-reliability environments, the difference between a smooth acceptance and a costly dispute is often documentation quality. For 25373994391, maintain a receiving record that includes:
- Purchase order reference and quantity
- Supplier name and shipment details
- Manufacturer and revision details (as provided by supplier and as shown on labels/markings)
- Inspection results and sampling method
- Any nonconformities and disposition actions (quarantine, return, rework, supplier corrective action request)
- Document set received (CoC/CoA/test reports/compliance declarations), including document IDs and dates if provided
This record supports internal QA review, production traceability, and audit readiness. It also supports financial resolution if there is a mismatch between what was ordered/accepted and what the supplier delivered.
To make the paper trail defensible, your records should be structured so that a third party can reconstruct decisions. In other words, avoid “notes without evidence.” Instead:
- Record the exact documents received and where they are stored.
- Link inspection outcomes to specific lots/serials and to your internal acceptance decision.
- Document deviations clearly: what you observed, which acceptance criteria were impacted, and what resolution path you used.
Also, consider that receiving documentation is frequently requested long after the purchase. The more consistent and complete your record-keeping, the less friction you will face later when investigating customer issues or audit findings.
Where localization fits: procurement in “nearby” contexts
The prompt includes a rule: “Anytime {city} or {country} appears in keywords, replace it with ""nearby.""” Since no explicit city/country placeholders appear in the provided keywords, the localization guidance is applied conceptually: many buyers operate within local distributor networks and regionally supported logistics. In such “nearby” procurement setups, lead times can look stable, but documentation and revision alignment can be the real differentiator. You should still validate identity and revision, even when a supplier is geographically convenient—because procurement risk does not vanish simply due to shorter shipping routes.
There is also a subtle risk with “nearby” procurement: regional convenience can encourage faster purchasing cycles, and faster cycles can tempt teams to skip the deeper verification steps. A good practice is to keep receiving verification steps consistent, regardless of shipping distance.
In fact, many organizations implement a “fast track” purchase workflow for low-risk items—but for critical identity-controlled parts, you should keep at least the identity checks and documentation review mandatory even in expedited lanes. If you want to accelerate, accelerate the process of verifying—don’t accelerate the process of skipping verification.
Comparison table: procurement strategies for 25373994391
The following table compares common approaches and their practical conditions. No external links are included.
| Approach | Top Use Case | Key Conditions / Requirements | Main Risks If Skipped |
|---|---|---|---|
| Number-first ordering (identifier-led) | When your internal system maps 25373994391 to a controlled spec | Require datasheet/revision confirmation; ensure mapping is controlled in ERP | Variant drift, revision mismatch, receiving disputes |
| Specification-first ordering (bundle-led) | When you need strict conformance across electrical/mechanical/compliance attributes | Define acceptance criteria; request manufacturer/datasheet revision alignment | Overlooking packaging or lot traceability needs |
| Supplier-validated ordering (document-led) | When contracts/audits require document retention and defensibility | Require CoC/CoA; lock RMA terms; confirm identity beyond the number | Limited traceability, audit gaps, costly rework |
| Hybrid approach (identifier + verification) | Very real-world production procurement workflows | Use 25373994391 to anchor the order; validate specs during receiving | Process inefficiency if sampling is not defined |
In many organizations, the hybrid approach is the most scalable because it reduces friction while keeping quality gates intact. You use 25373994391 to reduce catalog ambiguity, then you treat the supplier’s documents and your receiving tests as the actual proof of identity and conformity.
Step-by-step guide: ordering to acceptance for 25373994391
This is a structured workflow used by quality-minded procurement teams. Adapt the sampling intensity to your criticality level.
- Confirm your internal requirement: record the expected manufacturer, revision, and key specs tied to 25373994391.
- Ask for supplier confirmation: request a quotation that explicitly states manufacturer, part revision, and datasheet reference.
- Lock commercial terms: confirm price basis, quantity breaks, lead time, incoterms, and return conditions.
- Define acceptance criteria: outline which inspections/tests will be performed at receiving and what constitutes pass/fail.
- Issue the PO with traceability fields: include any required lot/serial information and acceptance references.
- Receive and inspect packaging: quarantine if packaging is damaged or seals are broken.
- Verify identity: check label-to-PO consistency and confirm manufacturer/revision markings.
- Perform sampling tests: validate electrical/mechanical parameters against the approved datasheet.
- Document results: record inspection outcomes and link results to the receiving lot.
- Release with traceability: only release parts when identity and spec conformity are established.
- Handle nonconformities: initiate RMA or corrective actions based on pre-agreed terms.
To make this workflow robust, you should also add “go/no-go decision points” where the receiving team has clear authority to stop the process. Without explicit authority, receiving teams sometimes hesitate to quarantine because they fear delays. The contract and the internal procedure should empower them to quarantine when identity markers mismatch or when required documentation is missing.
Also consider that acceptance criteria should be linked to risk. For example, if 25373994391 is used in a safety-critical function, you may require 100% inspection for specific properties or require full documentation sets for each lot. If it is a low-risk spare, you might reduce sampling intensity while still maintaining identity and traceability gates.
Industry context: traceability and quality controls (objective background)
Procurement systems increasingly rely on part identifiers for traceability, inventory control, and configuration management. In electronics, automotive, medical device supply chains, and other regulated or quality-critical industries, the challenge is rarely “finding a number that matches,” but rather ensuring that the item delivered is the correct revision, configured for the intended manufacturing environment, and supported by traceable documentation.
Quality assurance organizations and standards bodies emphasize traceability, documentation, and verification as fundamental pillars of dependable supply. For example, ISO 9001 (quality management systems) highlights the need for controlled processes, document retention, and systematic verification. Additionally, industry quality standards related to supply chain management often encourage supplier evaluation, risk assessment, and acceptance criteria definition. While the specifics depend on your sector, the underlying principle is consistent: procurement must be auditable and reproducible.
Another common industry practice is supplier qualification and periodic re-qualification. If you repeatedly receive nonconforming items or documentation gaps for 25373994391, your procurement response should evolve beyond receiving inspection. You may need to:
- Update supplier evaluation scores based on nonconformance rates.
- Increase inspection sampling for that supplier.
- Request corrective actions (CAPA) and verify closure evidence.
- Revisit your approved supplier list or channel authorization.
In mature quality organizations, procurement and quality are not separate silos. Purchasing affects quality because it determines what goods are supplied; quality affects purchasing because it determines what is acceptable and what is returned. Using 25373994391 as a traceability anchor should therefore integrate with both teams.
Note on statistics: Your prompt did not include verified numerical claims, and I will avoid inserting unverified performance metrics. If you share your industry (e.g., electronics components, industrial spares, medical devices), I can align this guide with the very relevant published guidance from recognized bodies.
FAQs
FAQ 1: Is 25373994391 the actual manufacturer part number?
Not necessarily. In many workflows, numeric strings like 25373994391 can be internal inventory identifiers, ERP SKUs, warehouse references, or catalog mapping keys. For reliability, confirm the manufacturer part number, revision, and datasheet alignment during supplier confirmation and receiving.
Even when a supplier says the code is the manufacturer part number, you should still verify it by checking whether the delivered part’s markings and the provided datasheet reference match. If there is any ambiguity, treat the identifier as a procurement key that must be resolved to the manufacturer’s controlled identifier.
FAQ 2: What documents should I request for 25373994391?
At minimum, request a quotation that states manufacturer and revision, plus receiving-relevant documentation such as a certificate of conformity or certificate of analysis (as applicable). For regulated or high-criticality contexts, request test reports/inspection certificates and any required compliance declarations.
Depending on the part type and your sector, you may also need:
- Material traceability documents (lot/batch details).
- Safety or regulatory compliance evidence relevant to your jurisdiction.
- Packaging compliance statements if special handling is required.
- Any change notification (if the supplier indicates revision changes prior to shipment).
The key is to make the document set a contract expectation where possible, not a discretionary request. Otherwise, documentation gaps can become a reason for acceptance delays or audit findings.
FAQ 3: How do I verify identity without relying on the number alone?
Use a combination of label-to-PO matching, physical inspection (dimensions, interfaces), and functional sampling tests. Then reconcile these with the approved datasheet and revision you already have on record.
If your part is embedded into assemblies, you may need a higher level of verification. For example, you might validate that the delivered part fits and performs in the first assembly test step, not just as an isolated component. But even in assembly contexts, you should still preserve lot-level traceability so you can backtrack if failures occur.
FAQ 4: What if the supplier claims compatibility for 25373994391?
Compatibility is not the same as conformity. If the item is not the approved manufacturer/revision, require a documented approval process (engineering/QA change control). Otherwise, the risk includes performance variance, compliance gaps, and disputes during warranty or customer claims.
In a disciplined system, you should require evidence for compatibility claims, not just verbal assurance. Evidence might include:
- Datasheet equivalency comparison (with explicit parameter mapping).
- Revision change justification and impact assessment.
- Test results that demonstrate meeting acceptance criteria for your application.
Also, clarify whether the supplier’s “compatibility” claim includes packaging/handling assumptions. Some replacements are electrically similar but are packaged differently, which can create environmental stress risks (especially for moisture-sensitive components) or ESD risk.
FAQ 5: How should I handle price differences for the same identifier 25373994391?
Price differences can reflect quantity breaks, lead time, packaging format, or sourcing route. Require clarity on pricing basis and include all relevant assumptions in your PO. If a supplier cannot specify the basis (e.g., quantity ladder or packaging), treat the quote as incomplete until clarified.
Price differences can also hide differences in product certainty. For example, a lower price might be associated with:
- Different revision (or unspecified revision).
- Different manufacturer site.
- Different packaging (e.g., not tape-and-reel suitable for your line).
- Different compliance documentation scope (e.g., missing CoC/CoA).
- Different return rights or restocking terms.
To protect against mis-buys, you should treat price clarity and identity clarity as equally important requirements.
FAQ 6: What are common causes of receiving failures?
The very common causes are revision drift, variant mismatch, packaging/handling issues, and insufficient documentation. A disciplined intake checklist linked to 25373994391 plus spec verification usually prevents the majority of avoidable failures.
Other receiving failures include:
- Incorrect lot traceability: labels missing or not matching paperwork.
- Damaged goods: packaging collapse, torn reels, moisture indicator issues.
- Partial shipments: delivered quantity differs and replacement does not match the original documentation.
- Obsolete component confusion: supplier ships a similar but outdated revision.
Because these failure modes are predictable, you can build specific checks into your receiving plan rather than using generic inspection language.
FAQ 7: Do I need a separate inspection plan for each supplier of 25373994391?
Typically, yes—at least to the extent that you verify manufacturer/revision alignment and adjust sampling intensity based on your risk assessment. Your acceptance criteria should remain consistent, while inspection sampling may be tuned to risk.
Supplier-specific inspection planning helps because each supplier has different reliability patterns and documentation quality. For example:
- A supplier with consistently correct documentation and traceability may require lighter sampling for non-critical parameters.
- A supplier with prior discrepancies might require stricter label verification and more frequent lot-level tests.
- A supplier operating through multiple channel layers might require increased documentation scrutiny and packaging verification.
Even when inspection intensity changes, the identity “gates” should generally remain non-negotiable for critical parts: if manufacturer/revision and label-to-PO matching are wrong, you should stop and quarantine regardless of sampling plans.
Concluding perspective: treat 25373994391 as the start, not the end
Procurement success with 25373994391 depends on disciplined validation: anchor the order to the identifier, but confirm identity and specification through documented supplier evidence and receiving verification. When you manage pricing clarity, supplier accountability, and traceable intake records together, you reduce disputes and protect downstream manufacturing quality—regardless of whether your supply chain is local, “nearby,” or distributed across regions.
If you provide the missing fields from your original prompt—specifically the supplier name(s), explicit price context, and any additional non-empty keywords—I can revise this guide to include those details precisely and tailor the QA checklist to the exact product category.
-
1
A Guide to Cost-Efficient Small Electric Cars for Seniors
-
2
Mastering Debt Consolidation: Boost Your Credit Score and Manage Interest Rates
-
3
Your Guide to Loans, Credit Checks, and Interest Rates
-
4
Affordable Independent Living: Finding the Right Senior Housing
-
5
Guide to Senior Living Apartments: Affordable and Comfortable Environments